Baoding Sitai Induction Heating Equipment Manufacturing Co., Ltd. is one of the leading manufacturers and suppliers of seamless calcium cored wire machine in China. We are committed to providing high quality customized products with competitive price. Welcome to contact us for quotation.
Production equipment for welded seamless pure calcium cored wire
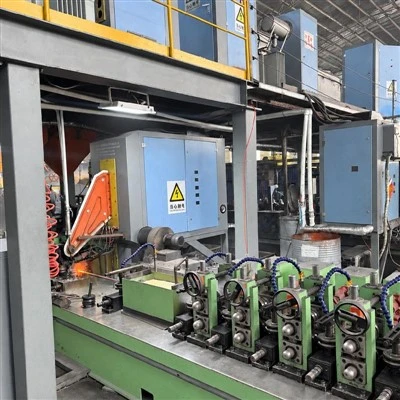
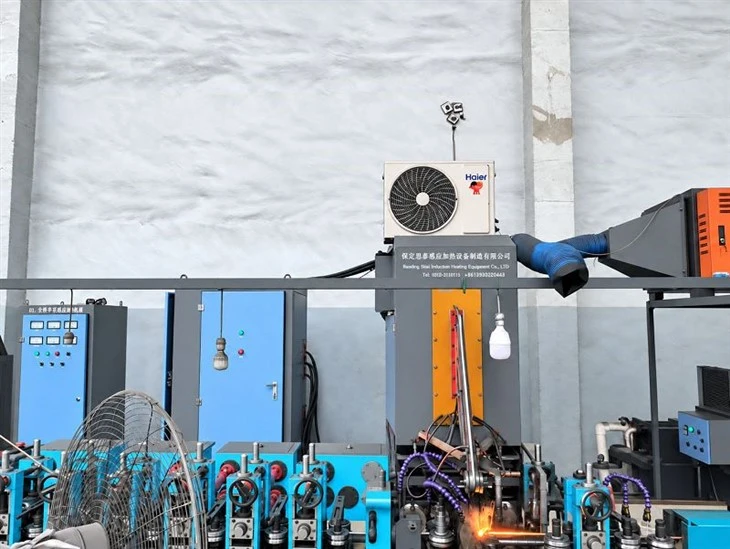
The SiTai Induction Seamless Calcium Cored Wire Machine forms steel strip around a solid calcium wire core and closes the longitudinal joint by high frequency welding. Subsequent sizing produces a continuously enclosed steel sheath for calcium treatment in secondary steel refining.
The production line focuses on weld integrity, wire dimensions and consistent core enclosure. These characteristics provide the manufacturing foundation for seamless calcium wire designed to improve calcium recovery and treatment consistency under suitable steelmaking conditions.
What seamless means
In this product, seamless describes a steel sheath with a continuously welded, closed longitudinal joint. The strip edges are metallurgically joined rather than mechanically locked. The wire is manufactured by forming and welding; it is not made from a seamless extruded tube.
Advantages of seamless calcium cored wire
Improved calcium recovery potential
A sound welded enclosure helps prevent premature opening of the sheath. When sheath thickness and wire feeding speed are matched to ladle conditions, calcium can be released deeper in the molten steel, helping reduce early calcium losses and improve utilization. Recovery depends on steel temperature, oxygen and sulfur levels, slag condition, bath depth and feeding practice; a fixed recovery percentage cannot be determined by the machine alone.
01
More consistent calcium addition
A continuous solid calcium core, controlled core diameter and consistent finished wire dimensions support a predictable calcium addition per metre. Together with stable sheath quality, these features help steelmakers control additions and reduce treatment variation between heats.
02
Better protection of the calcium core
Closing the longitudinal joint reduces a potential route for air and moisture to reach the calcium core during handling and storage. Protection depends on weld quality, wire ends, packaging and storage conditions. Finished coils still require dry storage and suitable moisture protection.
03
Stable wire feeding
A sound weld and controlled sizing help the wire retain its cross section during coiling, uncoiling and feeding. Consistent diameter, roundness and coil arrangement support smooth passage through compatible feed rollers and guides, reducing interruptions associated with deformation or joint opening.
04
Potential reduction in treatment cost
Where plant trials confirm improved calcium recovery, less added calcium may be needed to reach the same metallurgical target. The commercial benefit should be assessed as treatment cost per tonne of steel, considering calcium content, wire consumption and achieved steel quality.
05
How the production line works
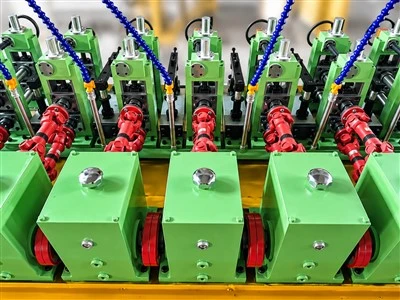
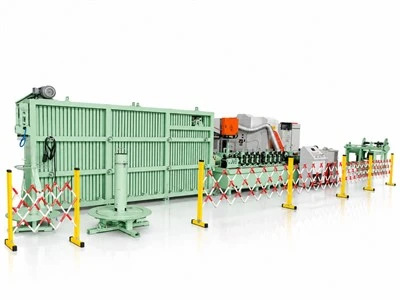
Steel strip is progressively formed around the solid calcium core. High frequency welding closes the longitudinal joint, followed by sizing, specified finishing stages and take-up. Annealing can be configured to suit the process.
Production line equipment
Finishing and auxiliaries
Annealing, straightening, take-up, traversing, finished wire coiling and water cooling, according to the selected configuration.
Steel strip handling
Vertical steel strip decoiler and accumulator for strip supply.
Calcium core handling
Vertical calcium wire decoiler and core guides.
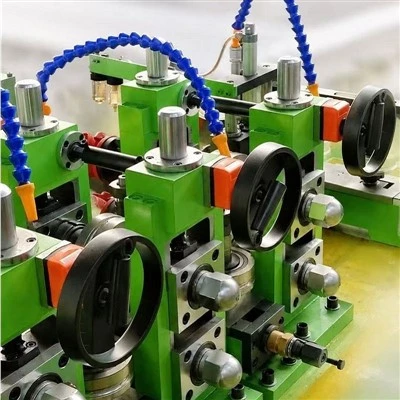
Roll forming and sizing
Roll passes configured for the specified strip and finished wire dimensions.
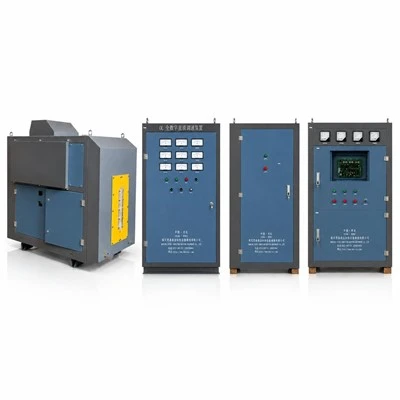
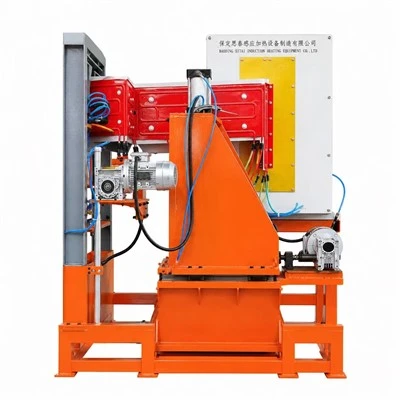
High frequency welding system
Rectifier, inverter and welding power supply integrated with the line process.
Configuration for your wire specification
|
Item |
Basis for configuration |
|
Finished product |
Welded seamless steel sheath with a solid calcium core |
|
Wire and core diameter |
Specified by the customer and checked against the forming route |
|
Steel strip width and thickness |
Selected for the sheath design and sizing sequence |
|
Welding power and production speed |
Matched to material dimensions and weld quality requirements |
|
Coil size and line layout |
Configured for handling requirements and available floor space |
SiTai Induction manufacturing capability
SiTai Induction integrates welding power supply development with equipment design, manufacturing, assembly and testing. Quality checks focus on weld continuity, dimensional consistency, core condition and coil formation.
Request a production line proposal
Send your finished wire diameter, calcium core diameter, steel strip specification, target speed, coil requirements and workshop layout. SiTai Induction will prepare a configuration for your seamless calcium cored wire project.
Frequently Asked Questions
Q: Why is this line described as a seamless calcium cored wire machine when the sheath is made from strip?
A: The word 'seamless' refers to the finished closed sheath: the longitudinal joint created from the formed strip is continuously welded so the two edges become metallurgically joined. It does not mean the sheath begins as an extruded seamless tube. This distinction is important because the production line combines strip forming with high-frequency seam welding to create the enclosed calcium-wire product.
Q: What is the advantage of using a solid calcium wire core instead of loose calcium powder?
A: A solid core provides a defined calcium cross section along the product length and avoids the powder-flow variation associated with a filled hopper. The line must still keep that core centered while the strip is formed and welded around it. Final metallurgical performance also depends on wire feeding practice, steel conditions and the integrity of the welded sheath, so the core form is only one part of the complete treatment result.
Q: Does a welded closed sheath automatically guarantee higher calcium recovery?
A: No single wire construction can guarantee a fixed recovery percentage in every steel plant. A sound closed sheath can reduce premature opening and help carry calcium deeper into the melt, but recovery is also influenced by steel temperature, composition, slag condition, injection depth, feed speed and the time between treatment and casting. The meaningful comparison is a controlled plant trial under the customer's own ladle practice.
Q: How are steel strip thickness and calcium-core diameter matched to the finished wire size?
A: The line is engineered from the requested finished outside diameter, solid calcium wire diameter and steel strip width and thickness. Forming passes create the enclosure, welding closes the joint and sizing brings the product to its final geometry. Changing one of these inputs can alter the available clearance and reduction schedule, so a new combination should be reviewed as a complete product drawing rather than adjusted by sizing rolls alone.
Q: What equipment is normally included in a complete seamless calcium cored wire line?
A: A project can include steel-strip payoff and accumulation, solid-calcium-wire payoff and guidance, roll forming, high-frequency welding, cooling, sizing, online annealing where required, straightening, take-up, traversing and final coiling. The exact boundary is agreed for each project. Listing the required automation and handling steps early prevents a quotation for the welding section from being mistaken for a turnkey line.
Q: How should weld integrity be checked during production?
A: Use a combination of continuous visual observation, dimensional checks and periodic samples that examine the longitudinal joint according to the customer's quality plan. A stable outside diameter does not by itself prove that the seam is sound. Process records linking strip, speed, welding settings and mechanical alignment make it easier to trace any defective section and reproduce an accepted condition.
Q: What should be tested during line acceptance with pure calcium wire?
A: Run the actual or agreed equivalent strip and solid calcium core through startup, stable production, speed changes and normal stopping. Check core centering, seam closure, final diameter, coiling behavior and the interaction between payoff, welding and take-up sections. Acceptance should use representative product for a sustained run rather than demonstrating each machine separately with no material.
Q: What information should a steelmaker provide before requesting a production-line proposal?
A: Provide the target finished wire diameter, solid calcium core diameter, steel strip dimensions and grade, required line-speed range, finished coil format, available plant power and cooling utilities, and factory layout constraints. If the wire must match an existing injection system, share feeder-roll and coil requirements as well. These inputs allow the line to be engineered around the actual treatment product and handling method.
Hot Tags: seamless calcium cored wire machine, China seamless calcium cored wire machine manufacturers, suppliers, factory