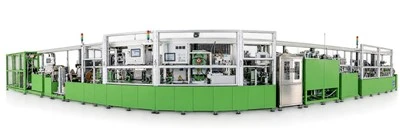
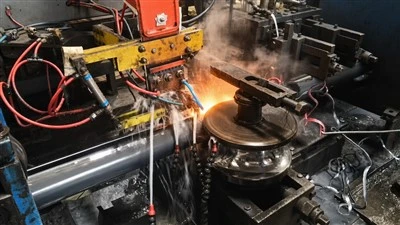
Surface Pre-treatment Equipment
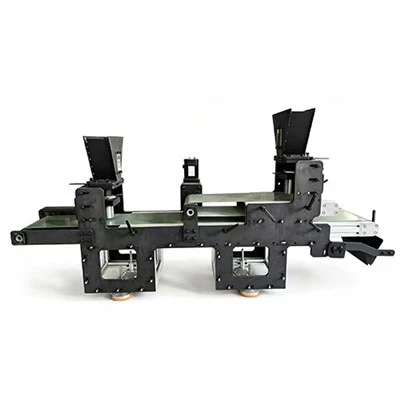
Copper-side Activation Station: Integrates a 120-grit automatic grinding mechanism and a 5% sulfuric acid activation bath; controls the welding surface roughness to Ra ≤ 1.6μm, generates a CuSO₄ transition layer conducive to filler metal adhesion, and thoroughly removes surface oxides and oil contaminants.
Aluminum-side Oxide Layer Removal Station: Equipped with a 10% NaOH alkaline cleaning bath (maintained at 60°C) and a mixed-acid pickling unit (20% HNO₃ + 5% HF); precisely breaks down the Al₂O₃ oxide layer (melting point 2,054°C) to create a microscopically roughened, activated surface.
Core Welding Units
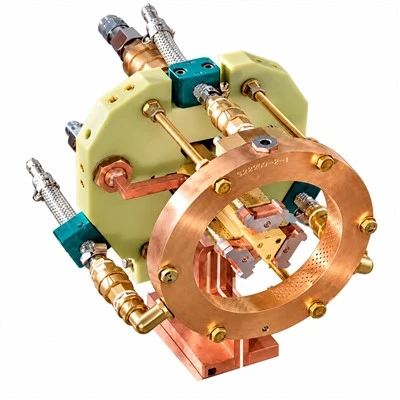
High-Frequency Induction Brazing Machine: Standard models feature 5–30 kW power and 30–100 kHz frequency; utilizes an asymmetric power output module (40% power to copper side, 60% to aluminum side) to maintain a temperature differential within ±20°C; completes brazing for tubes under Φ30mm in 5–7 seconds, offering 40% higher thermal efficiency than flame brazing.
Specialized Copper-Aluminum Resistance Butt Welder: Uses IGBT inverter control with current regulation precision within ±1%; supports a three-stage independent current cycle (preheat, main weld, temper); features a servo-driven pressure mechanism with a response time ≤ 30ms; achieves solid-state metallurgical bonding without filler metal; cycle time ≤ 4.2 seconds per piece.
Polymer Diffusion Welder: Employs molecular-level thermocompression diffusion technology; achieves weld strength exceeding 95% of the base material; suitable for high-precision applications such as new energy vehicle battery cooling tubes and copper-aluminum transition busbars; joint resistivity is lower than 0.02 μΩ·cm.