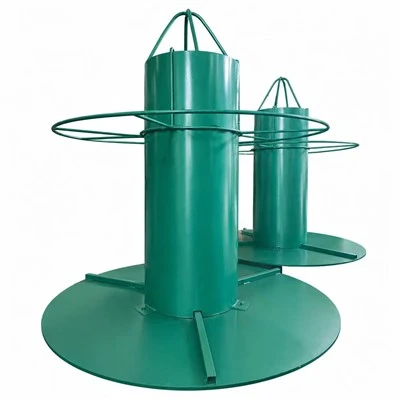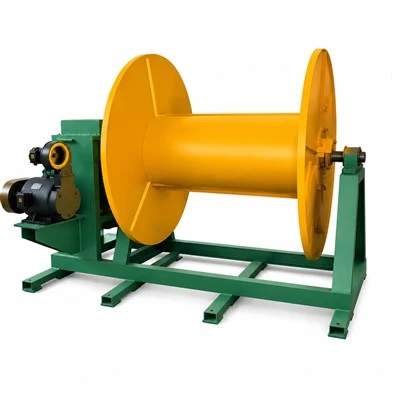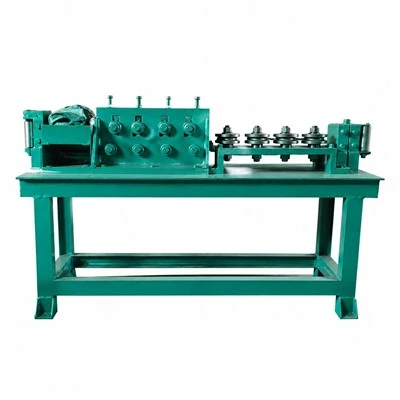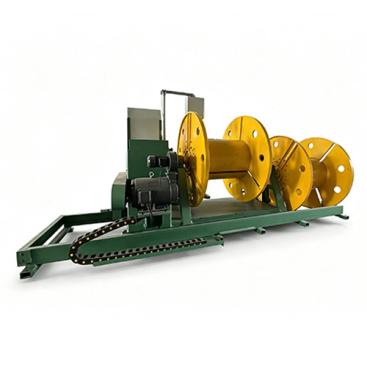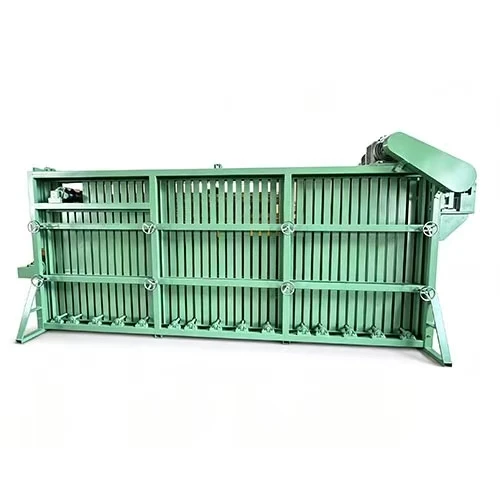
Baoding Sitai Induction Heating Equipment Manufacturing Co., Ltd. is one of the leading manufacturers and suppliers of vertical strip accumulator in China. We are committed to providing high quality customized products with competitive price. Welcome to contact us for quotation.
Continuous Strip Storage Solution for Stable and Uninterrupted Cored Wire Manufacturing
The Vertical Steel Strip Accumulator is designed for cored wire production lines to provide temporary strip storage and buffering during continuous operation. It is mainly installed between the strip pay-off unit and the forming section to maintain stable strip supply and reduce production interruptions caused by coil replacement.
With a vertical storage structure, the accumulator provides sufficient strip reserve space while occupying a compact installation area. It helps ensure continuous feeding of steel strip during coil changeover, improving production efficiency and the stability of the complete cored wire manufacturing process.
Main Features
Continuous Strip Feeding Buffer
The accumulator stores a certain length of steel strip in advance, allowing the production line to continue running during strip coil replacement and minimizing downtime.
01
Vertical Space-Saving Design
The vertical structure reduces floor space requirements while providing effective strip storage capacity, making it suitable for modern automatic cored wire production lines.
02
Stable Strip Tension Control
The guiding and buffering mechanism helps maintain smooth strip movement and stable feeding conditions, reducing strip fluctuation during high-speed production.
03
Reliable Mechanical Structure
The equipment is designed with a strong frame structure and durable components to ensure stable operation under continuous industrial working conditions.
04
Easy Integration with Production Lines
The accumulator can be connected with strip pay-off units, forming machines, filling systems, and other cored wire production equipment to improve overall automation performance.
05
Application
The Vertical Steel Strip Accumulator is mainly used for:
- Seamless cored wire production lines
- Welded cored wire production lines
- Metal powder filled wire manufacturing systems
- Continuous steel strip processing equipment
Technical Advantages
- Maintains continuous strip supply during coil replacement
- Reduces production interruption time
- Improves production line stability
- Compact vertical installation design
- Suitable for automatic continuous manufacturing systems
Customized Cored Wire Production Solutions
SITAI provides complete cored wire production line solutions, including strip pay-off units, steel strip accumulators, powder filling systems, welding equipment, sizing machines, annealing systems, straightening units, wire traversing systems, and finished wire take-up equipment.
According to different strip widths, material specifications, production speeds, and factory layouts, SITAI can provide customized accumulator designs to achieve efficient and reliable continuous production.
SITAI - Professional Manufacturer of Cored Wire Production Equipment and Industrial Automation Systems
Frequently Asked Questions
Q: How does a vertical strip accumulator reduce downtime during coil changes?
A: The accumulator stores a controlled length of steel strip while the upstream payoff and joining operation are handled. The downstream forming line can draw from this reserve for a limited period, giving operators time to complete the change without immediately stopping the process. The available buffer time is determined by stored strip length and the actual production speed, so it should be calculated for the intended changeover procedure.
Q: What determines the required accumulator capacity?
A: Start with the maximum time needed to stop the old coil, join or thread the new strip and restore normal payoff. Multiply that time by the planned downstream line speed, then include an operating margin and the physical limits of the accumulator. A larger storage tower is not automatically better; strip stiffness, available building height and the control response also influence a practical design.
Q: Why is strip tension important inside the accumulator?
A: The strip must remain controlled while moving through multiple guide points. Too much tension can stretch or deform thin strip and transmit load to the forming section; too little can create loops that contact the frame or run off a guide. The accumulator should isolate normal payoff disturbances from the downstream line while keeping the stored strip in a predictable path.
Q: What causes the strip to wander sideways in a vertical storage path?
A: Misaligned rollers, unequal guide heights, damaged strip edges or a payoff that enters the accumulator off-center can all create lateral movement. The correction should begin with the entry centerline and roller alignment rather than adding excessive side guides. Persistent edge contact can damage the strip and later disturb seam alignment in the cored wire forming section.
Q: How should the accumulator behave when it is nearly full or nearly empty?
A: The control system should define limits that prevent mechanical overtravel and give the upstream or downstream equipment time to respond. Near-full status may command the payoff to slow or stop; near-empty status may require the joining operation to finish or the main line to reduce speed. Alarm and interlock behavior should be tested during commissioning, not only during normal mid-range operation.
Q: Can the accumulator store different strip widths and thicknesses?
A: A range can be handled if roller width, guide geometry and bending radii remain suitable for all planned materials. Thicker or wider strip may require more force and a larger minimum bend radius, reducing the usable storage path. The complete product list should therefore be reviewed before the tower height and guide arrangement are fixed.
Q: What should operators check after a strip joint passes through the accumulator?
A: Observe that the joint travels smoothly over guides without catching, lifting or changing the strip centerline. If the joining method creates extra thickness, verify that the roller clearances can accommodate it. The joint should then be monitored until it reaches the forming section, where any local stiffness or edge mismatch can affect the product even though it passed through the storage tower successfully.
Hot Tags: vertical strip accumulator, China vertical strip accumulator manufacturers, suppliers, factory